LMES Standard Process Check-in Flow - Business Interaction Specification
1. Standard Check-in Interaction Flow
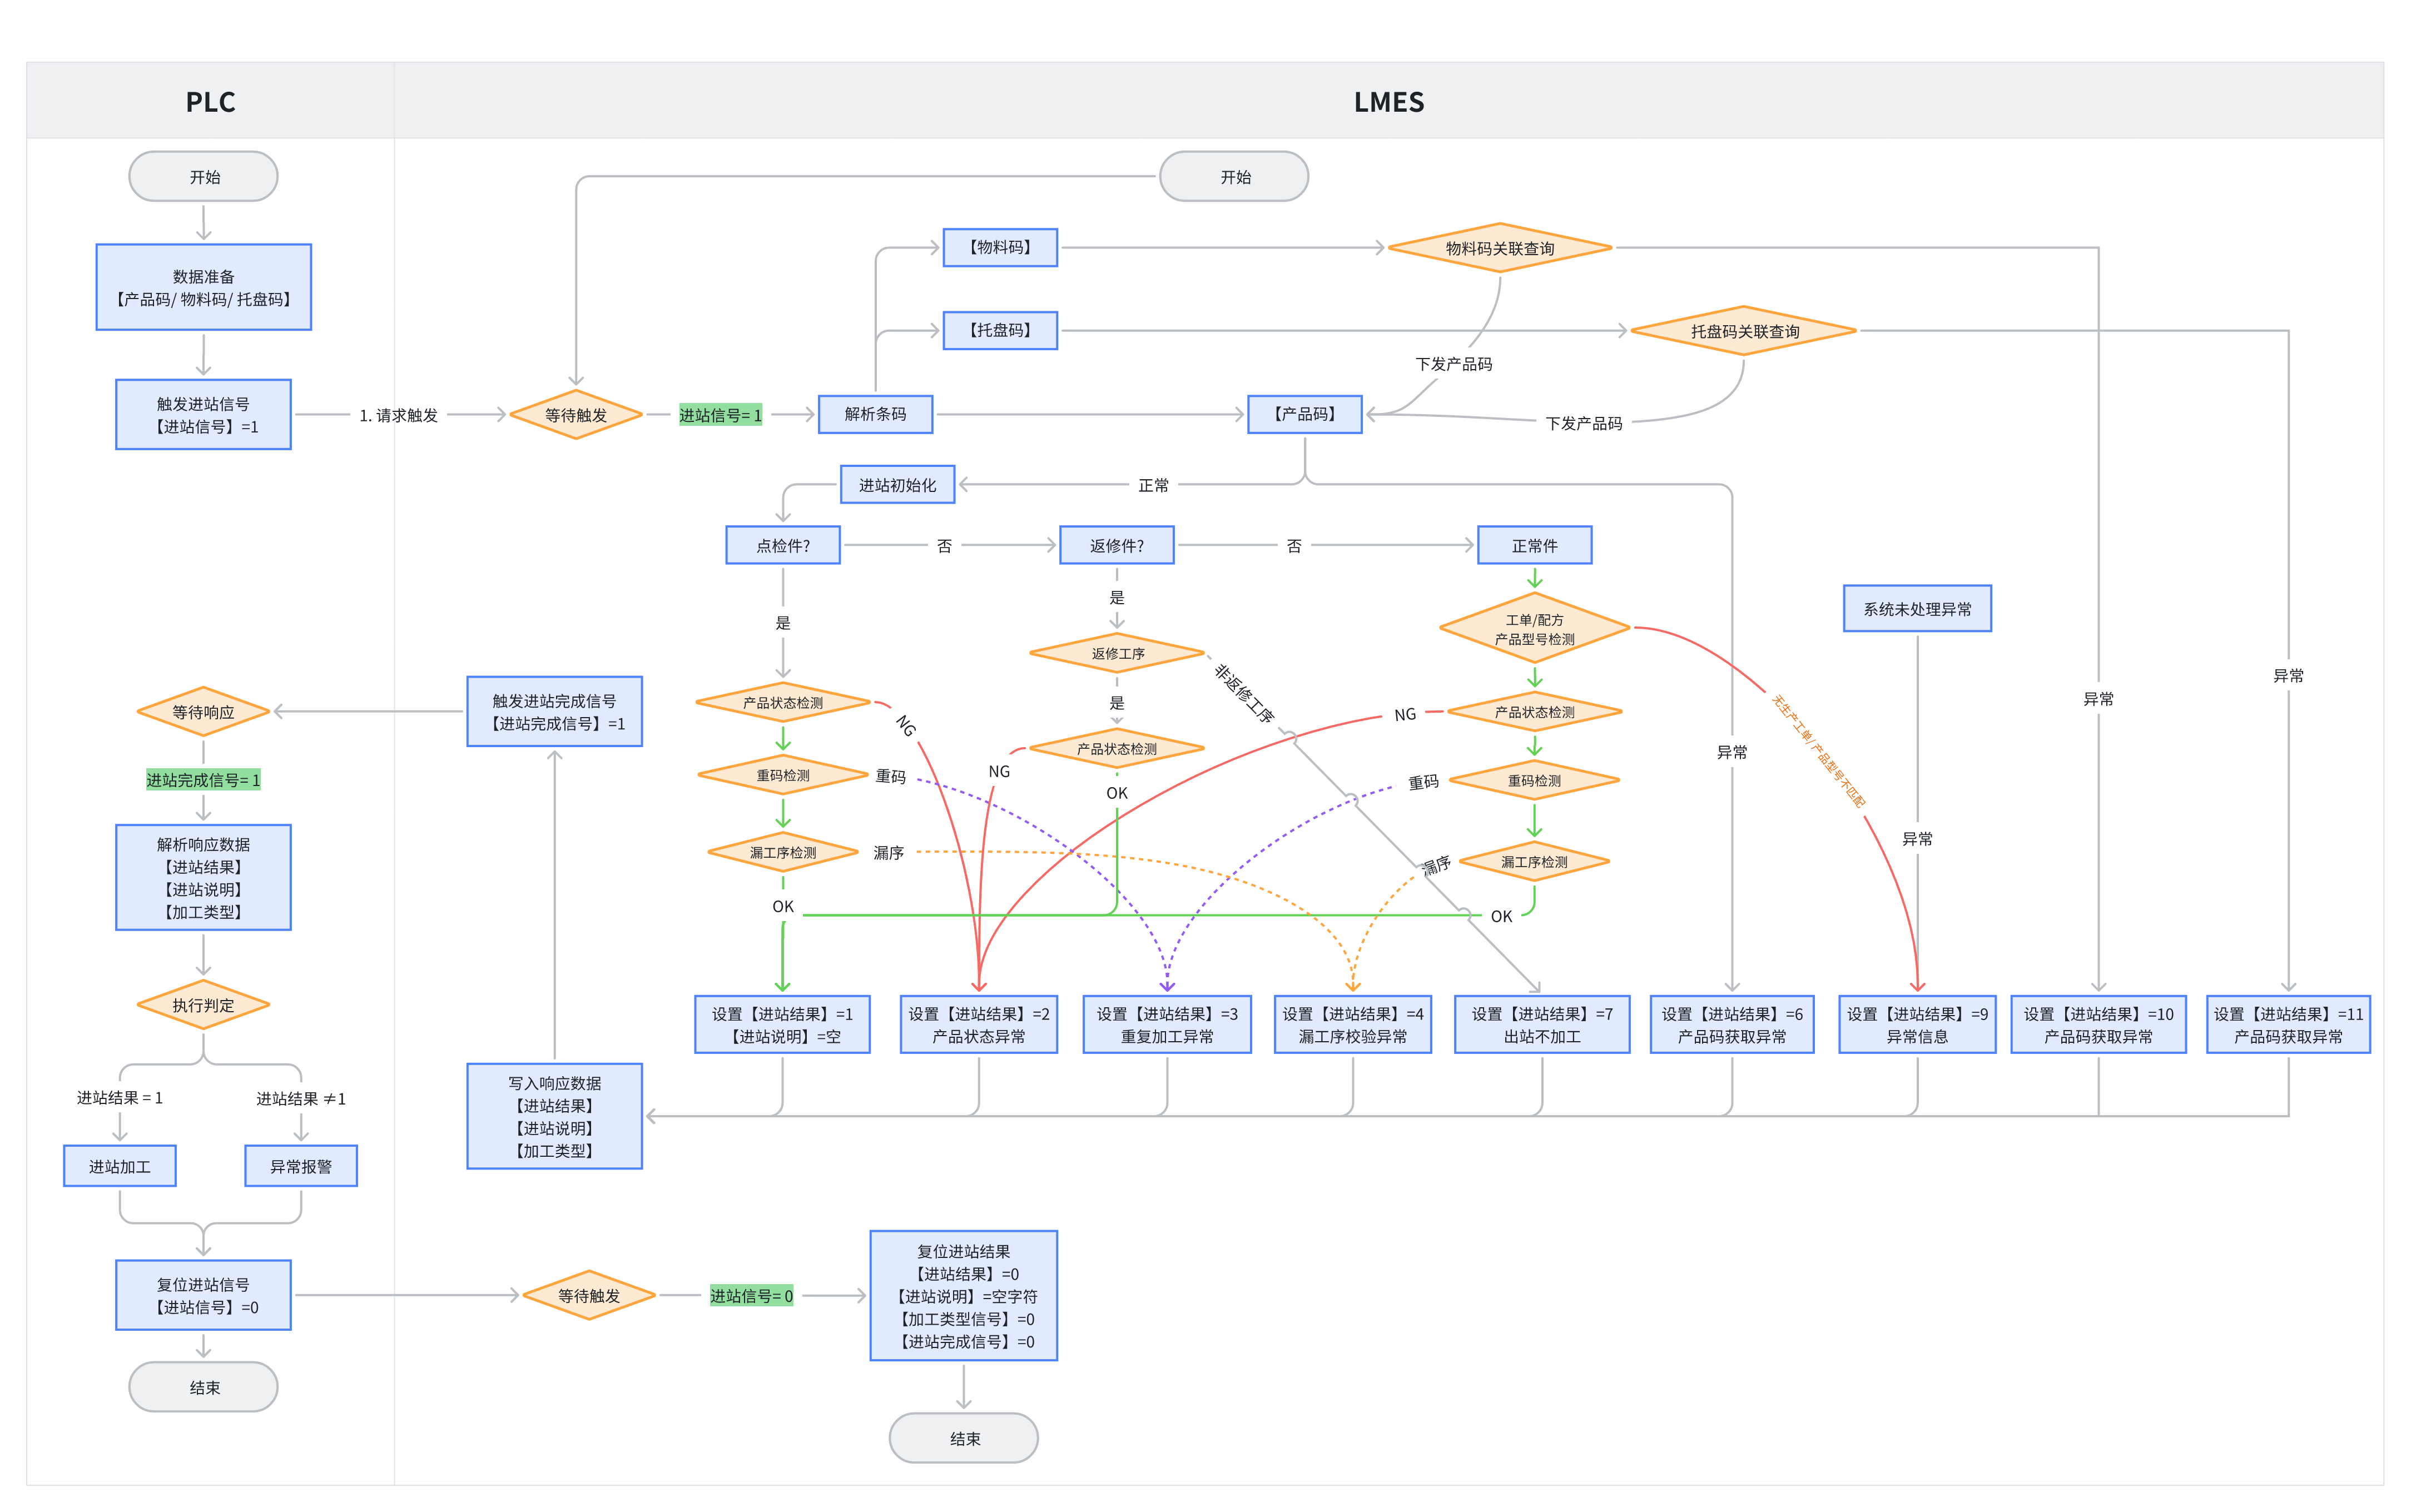
2. Interaction Variables and Result Codes
| Interaction Point | Direction | Data Type | Description |
|---|---|---|---|
| Check-in Signal | PLC -> LMES | Bool | Check-in signal. PLC sets to 1 to start the process. PLC is responsible for reset. |
| Product Code | PLC -> LMES | String | Check-in product serial number. Unique product identifier provided by PLC to LMES. |
| Material Code | PLC -> LMES | String | Check-in pallet code. Used when associating products through pallet code. |
| Pallet Code | PLC -> LMES | String | Check-in material code. Used when associating products through material code. |
| Check-in Complete Signal | LMES -> PLC | Bool | Check-in complete signal. LMES sets to 1 after processing is complete. LMES is responsible for reset. |
| Processing Type | LMES -> PLC | Int | LMES sends down product processing type, indicating the product handling type (Normal/Inspection/Rework) |
| Check-in Result | LMES -> PLC | Int | Check-in result code. LMES informs PLC of the final status of this interaction, which is the most important result signal. PLC should execute corresponding operations based on this code: • 1: Success - Release product normally. • 2: Product Status Abnormal - Intercept product, trigger alarm, remove product from line. • 3: Product Duplicate Code Abnormal - Intercept product, prevent repeated processing. • 4: Product Missing Process Abnormal - Intercept product, prevent products with missing processes from flowing in. • 5: MES System Abnormal - Pause line, wait for recovery, MES system fault handling • 6: Product Code Abnormal - Failed to get product code or product code is empty. Recommend alarm and pause line, wait for manual handling. • 7: Check-out No Processing - Product checks out but not processed, release to buffer area, special handling process. • 9: Other Abnormal - Unknown error occurred within system. Recommend alarm and pause line, wait for manual handling. •10: Material Code Not Bound - PLC provided material code, but system cannot find corresponding product. Recommend alarm. •11: Pallet Code Not Bound - PLC provided pallet code, but system cannot find corresponding product. Recommend alarm. • 0: Reset - After interaction is complete, LMES will reset this signal to 0. |
| Check-in Description | LMES -> PLC | String | Result description. When an exception occurs, LMES can write more detailed text description. |
3. Exception Troubleshooting Guide
When exceptions occur in the check-in process (such as product not released, equipment alarm), please follow these steps for troubleshooting.
Step 1: Check LMES Feedback Signals
First check the two key result variables written by LMES to PLC:
- Check-in Result: This is the most direct fault code.
- If the value is any value other than 1 (such as 2, 3, 4, 5, 6, 7, 9, 10, 11), it indicates that LMES encountered an error while processing business. Please refer to the description of the check-in result variable in the previous section to locate the problem cause.
- Check-in Description: This is the most useful troubleshooting information.
- When an exception occurs, LMES will write detailed, readable error text into this variable. For example, "Material code XXXXX not bound to product". Please display this variable content on the HMI or monitoring interface.
Step 2: Verify Signal Handshake Process
If LMES feedback signals appear normal, but the process is still stuck, please verify whether the standard "handshake" timing is complete. Non-standard signal states are potential sources of problems.
- Is Complete Signal set to 1?
- If PLC has not set this signal to 1, LMES will not start the process.
- Is Check-in Complete Signal set to 1?
- If PLC has requested, but this signal has not been set to 1, it indicates that LMES internal logic may still be processing or a serious error has occurred. At this time, focus on checking the content of Check-in Description.
- Has Complete Signal been reset to 0?
- According to the principle of "whoever triggers, whoever resets", this signal must be cleared by PLC. If the PLC program fails to clear it, although LMES is compatible with this abnormal situation to ensure line operation and can start new processes, this non-standard state is the root cause of potential problems and must be corrected in the PLC program.
- Have Check-in Complete Signal and other LMES signals been reset?
- At the end of the interaction, LMES should reset all signals it triggered. If these signals remain at 1, they may interfere with the judgment of the next check-in request or generate warnings in the LMES log.
Step 3: Use LMES Workstation Console
If more detailed information is needed, please use the Workstation Console function provided by the LMES system.
- Real-time Variable Monitoring: Can see the current values of all interaction points in real-time.
- Process Logs: Can see detailed business execution steps, locate which specific step the problem occurred.
- Warnings and Errors: Will highlight all error and warning information.
Step 4: Special Scenario Troubleshooting
Product Model Mismatch
- Error Types
- Recipe Product Model Mismatch: Product historical model ≠ Process applied recipe product model
- Order Product Model Mismatch: Product historical model ≠ Process segment order required product model
- Troubleshooting Steps
- Confirm Type: Check Recipe Distribution Method
- Method 0 (Only orders can be distributed): The system must be able to obtain the order issued by the current process segment and determine the product model accordingly. If there is no order, check-in is prohibited.
- Method 1 (Only process recipe can be distributed): The system relies on the recipe applied to the current process to determine the product model.
- Method 2 (Distribute when process identifies product): The system relies on the recipe applied to the current process to determine the product model. Ensure the recipe is correctly switched before check-in.